
Every component manufactured across our industrial forging lines conforms to rigorous ISO/TS 16949 tolerances. From companion flanges and steering king pins to heavy commercial brake units, our products undergo ultrasonic testing to thrive in heavy multi-axle freight operations.
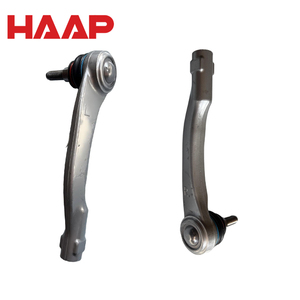
High-precision cold-forged ball studs with anti-fatigue induction treatment; engineered for zero-backlash dynamic steering stability.
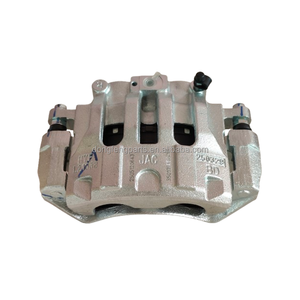
Ductile nodular iron housing with phenolic pistons; resistant to high-temperature hydraulic pressure spikes and stop-and-go glazing.
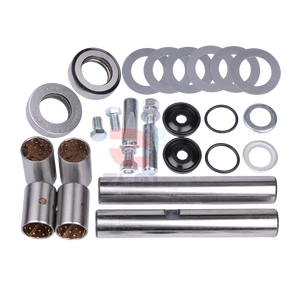
Precision ground 20Cr alloy steel pins with induction carburized case depth (1.8-2.2mm) to endure immense vertical steer loads.
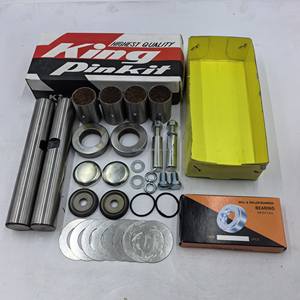
Complete king pin overhaul assembly featuring phosphor-bronze thrust washers and high-tensile retaining shims.
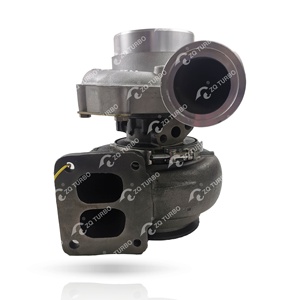
High-nickel turbine housing and precision balanced Inconel 713C rotor assembly handling exhaust flows up to 980°C.
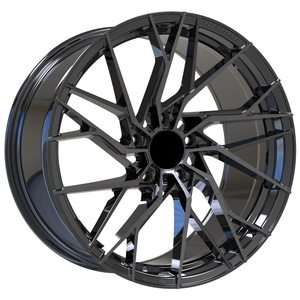
Forged T6-6061 aerospace alloy wheel barrels with optimized flange bead seats designed to decrease unsprung rotational mass.
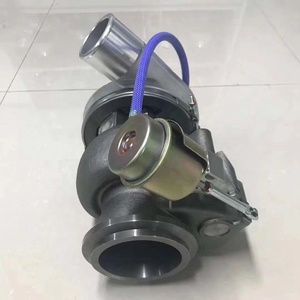
Heavy-duty 360° bronze thrust bearing package engineered for high continuous boost pressures in heavy mining and freight tractors.
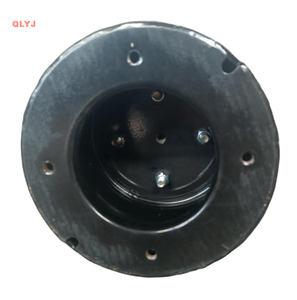
Multi-ply natural rubber bellows with reinforced synthetic cords and electrophoretic steel bead plates for intense articulation.
Commercial vehicle output flanges interface directly with the main transmission output shaft and the propeller shaft companion end. Operating under tremendous dynamic torsional shear and continuous cyclical shock loads, these critical forgings demand strict metallurgical integrity.
Unlike cast or flame-cut substitute parts that experience sudden brittle fracturing across the spline collar, our transmission output flanges are formed through 2500-ton closed-die drop forging. This process guides continuous metallic grain lines unbroken along the cross-sectional flange face and hub radius, yielding superior fracture toughness under full-throttle gross combination weight (GCW) conditions.
Drivetrain flanges must balance an ultra-hard internal spline interface with a ductile, shock-absorbing body. Our specialized CNC dual-frequency induction hardening machines treat internal involute splines to 58-62 HRC at a case depth of 1.5 to 2.5 mm, while retaining a core hardness of 28-32 HRC. This dual-hardness zone completely prevents premature spline fretting without risking catastrophic brittleness.
High-speed driveline vibration is the primary driver of transmission output seal failure and gearbox casing cracking. Our companion output flanges are machined on high-precision CNC multi-axis turning centers and broached to DIN 5480, ISO 4156, and SAE standards. Flange face perpendicularity and radial runout are maintained below 0.015 mm, eliminating harmonic vibration.
Operating commercial vehicles across Greater Mumbai, Navi Mumbai, and the Konkan hinterland imposes severe stresses found in few other places worldwide. Our output flanges and powertrain components are engineered specifically to overcome these localized operational threats.
The Jawaharlal Nehru Port Trust (Nhava Sheva) generates over 5 million TEUs annually, creating heavy container trailer backlogs along the Panvel-Uran and Thane-Belapur expressways. Multi-axle tractor-trailers (40 to 55-ton GCW) experience relentless stop-and-go low-gear torque spikes for hours at a time. Standard flanges suffer micro-fretting corrosion on splines under this continuous low-frequency shock.
Traversing the Mumbai-Pune Expressway (Bhor Ghat) and the Mumbai-Nashik highway (Kasara Ghat) forces heavy commercial vehicles up sustained 1:12 gradients. At extreme throttle and elevated transmission oil temperatures (often exceeding 120°C), driveline output flanges endure continuous peak torque, followed by immediate engine-braking torque reversals during descent.
Mumbai's 4-month Southwest monsoon season dumps over 2,200 mm of torrential rainfall combined with airborne saline humidity from the Arabian Sea. Road spray mixed with industrial particulates creates abrasive, highly conductive slurries. Normal steel flange oil-seal sleeves pit rapidly, destroying radial shaft seals and venting transmission oil.
The commercial transport sector in Maharashtra is experiencing rapid technological disruption. Fleet buyers in Mumbai are prioritizing uptime, reduced Total Cost of Ownership (TCO), and BS-VI driveline compatibility.
India’s nationwide enforcement of BS-VI emission standards equipped commercial fleets (Tata Signa, Ashok Leyland AVTR, BharatBenz) with high-pressure common rail engines delivering 20-35% higher peak low-end torque compared to older BS-IV platforms. This torque surge exposes legacy aftermarket output flanges to catastrophic shear. Mumbai fleet workshops require upgraded flanges certified for torque capacities exceeding 22,000 Nm.
Fleet operators serving the Mumbai-Pune-Ahmedabad industrial cluster are rapidly deploying automated manual transmissions to lower driver fatigue and boost fuel efficiency. AMTs execute rapid, automated clutch actuations that generate crisp, high-frequency torque transitions. Output flanges with imprecise spline clearances fail under rapid gear hunting; zero-backlash broached flanges have become an essential replacement standard.
The warehousing clusters of Bhiwandi and Taloja have consolidated into massive automated logistics parks. Operators are switching from older 2-axle rigid trucks to multi-axle tractor trailers (3523, 4028, and 55-ton platforms). Unscheduled vehicle downtime costs fleet operators up to 15,000 INR per day, prompting fleet managers in Mumbai to bypass unreliable local casting remakes in favor of precision forged imports with verified mill certificates.
With the Brihanmumbai Electric Supply and Transport (BEST) undertaking expanding its electric bus operations to thousands of units and JNPT transitioning to electric terminal shunting tractors, EV drivelines are arriving rapidly. Electric motors deliver 100% instant torque at zero RPM, putting extreme shear loads on companion drive flanges. Our high-tensile forged flanges directly support high-torque EV gearbox outputs.
Clear, practical technical and commercial answers regarding customs clearing at JNPT Nhava Sheva, BIS compliance, material validation, and logistics consolidation.
Shipments destined for Mumbai import through Jawaharlal Nehru Port (JNPT) or the Mumbai Air Cargo Complex under HS Code 8708.99.00 (Parts and accessories of motor vehicles) or 8708.29.00. Clearance requires standard shipping manifests: Commercial Invoice, Packing List with detailed net/gross weights per pallet, Bill of Lading (Clean on Board), and Certificate of Origin.
Our export documentation team pre-files electronic declarations, ensures GSTIN matching, and attaches detailed OEM cross-reference sheets to prevent customs verification delays at inland container depots (ICDs) such as Mulund or Dronagiri CFS.
Yes. Automotive safety and structural integrity in India are regulated under Automotive Industry Standards (AIS) and Bureau of Indian Standards (BIS) specifications. Our forged transmission components and flanges comply fully with dimensional, metallurgical, and dynamic endurance benchmarks aligned with AIS-037 and ISO/TS 16949 standards.
We provide full EN 10204 3.1 chemical composition certificates and destructive test reports with every bulk production batch, assuring compliance with OEM factory benchmarks.
We maintain an extensive OEM cross-reference database for Indian commercial platforms, including Tata Motors (G600, G1150 gearboxes), Ashok Leyland (ZF 6S, 9S gearboxes), BharatBenz, and European heavy haulers (Volvo, Scania, Mercedes Actros). We cross-check key engineering parameters before production:
1. Spline specification (e.g., DIN 5480 spline tooth profile, pressure angle, and pitch diameter);
2. Flange bolt circle diameter (PCD), bolt hole count, and serration pitch (cross-serrated KV120, KV150, or flat companion design);
3. Oil-seal journal diameter and overall axial stack height.
Direct ocean freight services from Ningbo or Shanghai port to JNPT Nhava Sheva have an average transit time of 14 to 18 days, making ocean freight fast and economical. We support both FCL (Full Container Load) and LCL (Less than Container Load) shipments.
For distributors sourcing mixed items, we consolidate output flanges, king pin kits, turbochargers, brake chambers, and suspension bags into unified shipping units, treated with VCI anti-corrosion barrier packing and palletized in ISPM-15 heat-treated wooden crates.
For standard catalog configurations with ready tooling, our typical MOQ is 50 to 100 units per reference. For specialized customized companion flanges tailored to non-standard axle adaptations, MOQs start from 200 units.
We supply sample units by air express (DHL/FedEx directly to Mumbai or Pune workshops) within 5 business days for CMM coordinate measuring verification, dyno testing, and trial installation before commercial batch release.
Driveline flanges feature high-precision ground seal journals and machined splines that are highly vulnerable to oceanic condensation and Mumbai’s coastal air. All finished steel surfaces receive multi-stage phosphating followed by high-grade Cortec VpCI rust-preventive oil coating.
Each unit is individually sealed in heat-fused VCI vapor-corrosion-inhibitor polythene bags with active desiccant packs, then packed in heavy-duty cardboard cartons before shrink-wrapping on fumigated pallets, guaranteeing pristine condition upon warehouse arrival.
Integrating large-scale automated forging with precision CNC machining, we deliver robust drivetrain components directly to international transport markets with unmatched consistency.
Operating friction screw and automated hydraulic drop-forging presses ranging from 1,600 to 4,000 tons, our facilities produce over 120,000 precision commercial vehicle drivetrain forgings monthly. Closed-die forging ensures high structural density, eliminates internal porosity, and yields superior fatigue limits compared to ductile iron casting alternatives.
Every single output flange undergoes wet horizontal magnetic particle inspection (MPI) under ultraviolet light to verify total absence of sub-surface micro-cracks along the critical neck-to-face transition radius. In addition, our climate-controlled metrology laboratory utilizes ZEISS 3D coordinate measuring machines (CMM) to maintain sub-micron dimensional compliance.
With an experienced export documentation and logistics desk handling trade compliance across South Asia, the EU, and the Middle East, we streamline CIF, FOB, and DDP contracts. Direct ocean carriers connect our production hubs to Nhava Sheva within 18 days, minimizing inventory carrying costs and stock-out risks for our Mumbai distributor partners.
Whether you require standard ZF, Eaton, Mercedes, Tata, or Scania companion output flanges, or need custom forging dies fabricated from your engineering sample, our engineering desk delivers technical feedback within 24 hours.
Inquire Now